The safest sourcing structure isn’t always the one with the most suppliers. In single-source vs multi-vendor medical device manufacturing, consolidating work can simplify quality oversight and change control, but it can also increase reliance on one partner. Distributing work may reduce that dependency, yet each handoff adds coordination and accountability requirements.
Both models can support a device portfolio when their risks are understood and controlled. The right choice depends on the device’s technical requirements, the strength of your supplier controls, and how much integration your team can manage. This comparison examines trade-offs in quality oversight, supply continuity, integration, and lifecycle accountability, then outlines the controls to consider before choosing a structure.
It also explains when an integrated CDMO may simplify coordination across development, engineering, manufacturing, assembly, and testing. Fong’s Engineering & Manufacturing provides end-to-end support for medical device projects, from concept and prototyping to validation and production. The goal is not to prescribe one model for every portfolio, but to help you identify the sourcing approach that fits your operational and lifecycle priorities.
Key Takeaways
- Define the supplier scope clearly: a single-source model can cover one stage or a broader lifecycle scope, while a multi-vendor model distributes defined work across suppliers.
- Compare single-source vs multi-vendor medical device manufacturing by assessing quality interfaces, supply continuity, coordination demands, and accountability for change control.
- Balance potential benefits against the controls they require, including contingency planning for supplier dependency and disciplined interface management across vendors.
- Choose a structure based on product scope, lifecycle stage, critical processes, and your team’s capacity to oversee suppliers and coordinate engineering changes.
- Consider whether an integrated CDMO can reduce handoffs across selected development and manufacturing stages, while keeping the partner’s scope aligned to portfolio needs.
Single-source vs multi-vendor medical device manufacturing: what each model means
The distinction is about how defined work is allocated, not simply how many organizations appear in a supplier list. Single-source manufacturing assigns a defined scope of work to one supplier; multi-vendor manufacturing distributes defined products, processes, or production stages across multiple suppliers. Neither structure is inherently safer. Suitability depends on the scope, interfaces, and oversight arrangements established for the device.
Scope matters because medical device development and production can span design work, components, process development, assembly, testing, and packaging. This Medical device manufacturing overview provides broad context: a device’s design and intended use shape the activities involved in producing it. The sourcing model determines how those activities and their associated responsibilities are organized.
What does single-source manufacturing cover?
Under a single-source arrangement, one supplier may perform a selected stage, such as component manufacturing, or coordinate a wider scope spanning development, manufacturing, assembly, and testing. The term does not mean that every task must sit with that supplier. The project agreement and quality documentation should specify deliverables, interfaces, decision rights, records, and responsibilities retained by the device company.
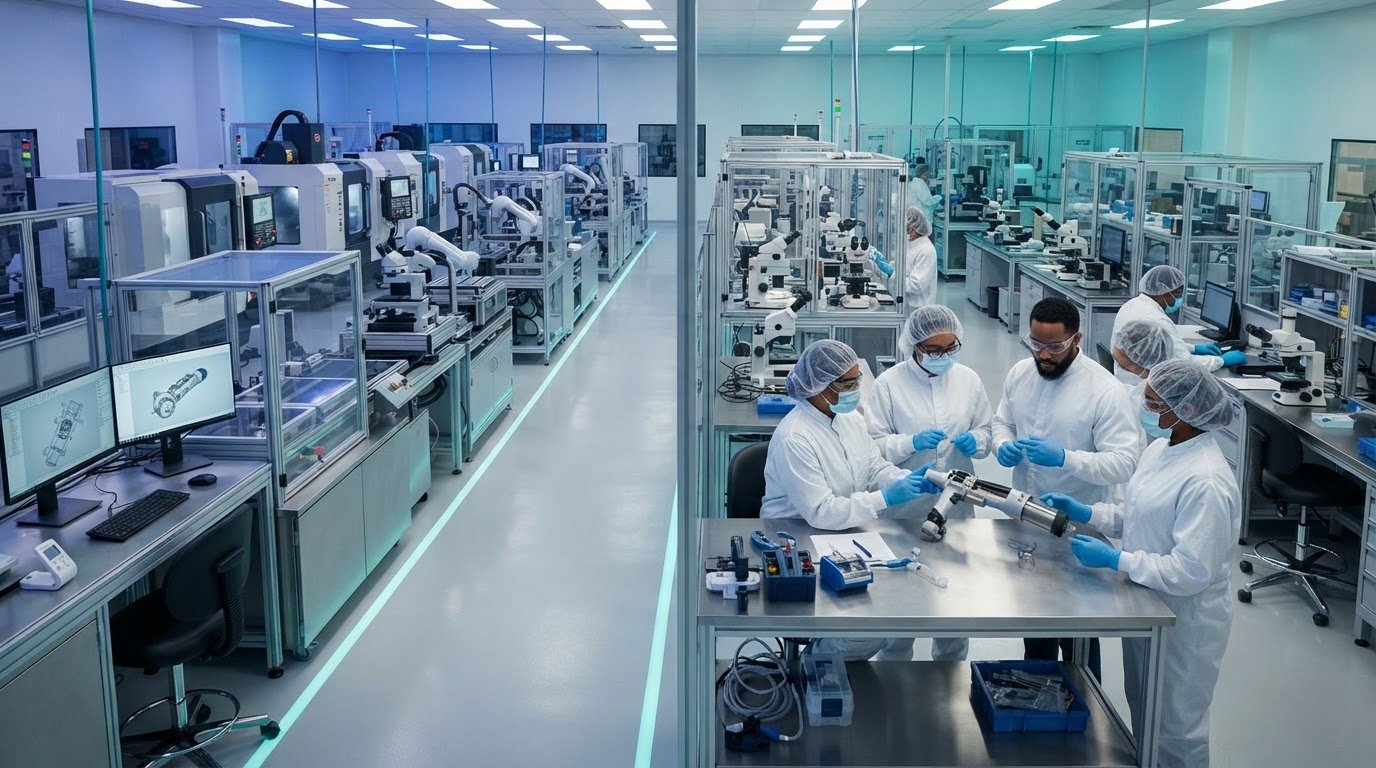
For example, Fong’s end-to-end CDMO capabilities can support work from concept and prototyping through validation, assembly, and production. Depending on the defined project scope, capabilities may include precision machining, laser processing, cleanroom assembly, testing, and packaging. This shows how one CDMO can cover multiple stages without implying that every project uses every capability. Clear boundaries remain essential, including who approves design changes and how information passes between teams.
What does multi-vendor manufacturing look like?
A multi-vendor structure assigns distinct work to separate suppliers. One company might manufacture components, another perform a specialized process, and a third assemble or test the finished device. The device company generally coordinates the interfaces: it must establish how specifications, samples, process records, nonconformance information, and change notifications move between organizations. Contracts and quality agreements should make responsibility boundaries explicit, especially when one supplier’s output becomes another’s input.
This model can also be blended. A lead CDMO may coordinate selected development and production activities while specialist suppliers provide defined components or processes. In that arrangement, the number of suppliers does not by itself show who manages the overall workflow. Clarify which activities the lead partner controls, which remain directly managed by the device company, and how shared decisions and records are handled.
For portfolio planning, map the work before labeling a program single-source or multi-vendor. List each product, process, and lifecycle stage, then identify the responsible organization and every handoff. This makes the model visible in operational terms and gives teams a practical basis for comparing supplier structures.
How supplier structure affects quality, continuity, and lifecycle control
Supplier structure shapes how quality information, decisions, and recovery actions move through a device program. A single supplier may reduce the number of direct interfaces, while a multi-vendor arrangement can distribute work across organizations with separate systems and records. Neither structure removes the device company’s need to define oversight. The practical question is whether responsibilities remain clear from incoming materials and process controls through finished-device release and later changes.
Quality oversight across one or several suppliers
Map each supplier’s responsibilities in the quality agreement and related procedures. Specify who controls approved specifications, reviews records, reports nonconformances, and communicates changes. For corrective and preventive action (CAPA), define who investigates a problem, provides evidence, approves actions, and verifies effectiveness. If a defect crosses a supplier boundary, establish how affected parties share information and coordinate containment.
Risk management, process validation, and record retention also need defined interfaces. For example, if one supplier manufactures a component and another assembles it, establish how component acceptance criteria and relevant process information reach the assembly team. The customer should retain visibility into the evidence needed for its own quality decisions. ISO 13485 provides a quality-management framework; alignment with it is not blanket approval of a product or a substitute for product-specific regulatory assessment.
Fong’s quality-system support includes an ISO 13485 quality system and process validation frameworks such as IQ, OQ, and PQ. In any sourcing structure, documented ownership helps teams connect validation evidence to the processes and responsibilities it covers.
Business continuity and concentration risk
Continuity depends on more than supplier count. A single-source arrangement may concentrate specialized knowledge, tooling, capacity, or process control in one place. A multi-vendor design may offer alternatives, but only if those suppliers can work to controlled specifications and their processes, materials, and outputs are appropriately qualified for the intended role.
Map potential single points of failure across the product’s critical processes and inputs. Consider whether production depends on unique tooling, a particular material, specialist expertise, or a shared upstream supplier. Then define contingency actions: who assesses the impact, who authorizes a transfer or substitute, and what validation or documentation is needed before production resumes. A second supplier is not an effective alternative if it relies on the same constrained input or cannot reproduce the controlled process.
- Capacity: Identify where available production capability could constrain recovery.
- Dependencies: Trace critical components, materials, tooling, and specialist processes beyond the direct supplier.
- Recovery ownership: Assign responsibility for communication, decisions, and evidence during a disruption.
Clear responsibility allocation is the foundation of effective lifecycle oversight, because every quality decision, change, and recovery action needs an accountable owner. For programs that need coordinated engineering, manufacturing, assembly, and testing, an integrated CDMO scope can reduce selected handoffs while keeping customer responsibilities explicit. Teams defining that scope can discuss their manufacturing requirements.
Single-source vs multi-vendor manufacturing: compare the trade-offs
The practical comparison is not a contest between fewer and more suppliers. It is an assessment of where coordination, dependency, and technical capability sit across a device program. In single-source vs multi-vendor medical device manufacturing, product complexity, specialized processes, and the customer’s internal expertise can shift the balance. A model that suits a mature product with stable processes may not fit a device still undergoing engineering changes.
| Consideration | Single-source | Multi-vendor |
|---|---|---|
| Coordination | Fewer direct supplier interfaces may simplify communication; defined escalation routes and customer oversight remain necessary. | More handoffs require active coordination, agreed specifications, and clear decision ownership. |
| Visibility | A supplier may provide a consolidated view across its assigned scope; visibility into subcontracted work still needs definition. | Information may sit across separate systems and records; shared reporting and documentation rules help connect it. |
| Dependency | Concentrates defined activities with one supplier, making contingency planning and dependency mapping important. | Distributes work, but suppliers may share upstream materials, tooling, or other dependencies. |
| Scalability | Expansion depends on the supplier’s capability and capacity for the required scope. | Specialist suppliers can add distinct capabilities, while qualification and coordination effort can grow. |
| Interface management | Fewer supplier-to-supplier interfaces may be needed, but internal handoffs and retained responsibilities must still be managed. | Each transfer needs controlled specifications, records, acceptance criteria, and change communication. |
Where a single-source model may fit
A single-source model may be useful when a defined package of engineering and manufacturing work benefits from close coordination. Any gains in interface simplicity depend on the scope actually assigned, not the supplier count alone. Set measurable performance criteria, escalation paths, change responsibilities, and continuity plans. Concentrated responsibility does not transfer the customer’s quality oversight or accountability for decisions affecting the device.
Where a multi-vendor model may fit
Multi-vendor sourcing may suit programs that depend on distinct specialist capabilities or require flexibility across defined activities. That flexibility comes with work: qualifying suppliers, controlling interface specifications, maintaining oversight, and coordinating changes across organizations. A lead supplier or formal governance process can clarify handoffs and route decisions, provided authority and responsibilities are documented rather than assumed.
Evaluate potential benefits alongside the conditions needed to achieve them. An integrated partner with engineering and manufacturing capabilities may reduce customer-managed handoffs across selected stages; Fong’s CDMO scope can be aligned to project needs. A distributed structure may provide access to specialized processes, but teams need sufficient expertise to govern supplier interfaces. Avoid assuming either arrangement will lower cost, accelerate delivery, or improve quality without evidence from the specific program. Compare process requirements, capacity, and oversight resources before selecting a model.
How to choose a sourcing model for a medical device portfolio
Choose the structure around the work your device requires and your organization’s ability to govern it. A portfolio may need different arrangements for different products or lifecycle stages. Use this framework to compare the options before assigning or transferring production.
- Define product scope and lifecycle stage. List the products, components, and activities in scope, from development and prototyping to validation, assembly, testing, and production. Distinguish current work from future needs, since a structure that fits a stable product may not suit one still undergoing design changes.
- Identify critical processes and interfaces. Map component dependencies, specialized processes, assembly steps, and acceptance points. Mark each handoff and record what information, materials, and quality records must pass between organizations.
- Assess technical complexity. Consider device architecture, component criticality, and process specialization. For a complex assembly, account for cleanroom requirements, testing, packaging, and validation interfaces. Ask whether the proposed supplier structure can coordinate these elements under the project’s defined controls.
- Measure internal oversight capacity. Determine whether your team can qualify suppliers, maintain quality oversight, coordinate engineering decisions, and control changes across every interface. A multi-vendor structure calls for capacity to govern supplier relationships; a single-source arrangement still requires clear customer decision rights and oversight.
- Map continuity risks. Identify dependencies in tooling, materials, capacity, processes, and specialist knowledge. For critical activities, decide whether a qualified alternative is needed or whether other contingency controls are appropriate. Account for shared upstream dependencies rather than treating supplier count as a measure of resilience.
- Set governance before committing. Define specifications, document ownership, change notification, escalation routes, acceptance criteria, and responsibility for qualification and validation evidence. Agree how risk reviews and production-transfer records will be controlled before work moves or is divided.
Match supplier structure to device and process complexity
Complexity can favor integrated coordination when engineering, manufacturing, assembly, and testing activities depend on close communication. Fong’s CDMO support can be aligned to selected lifecycle stages, with capabilities including cleanroom assembly, testing, and packaging. If assembly scope is central to the decision, include the required process controls and handoffs in the evaluation rather than counting suppliers alone.
Set governance before transferring or splitting production
A production transfer or split is a controlled change, not just a new purchasing arrangement. Define who approves specifications and revisions, who owns records, and what evidence is required to qualify the receiving process. Include validation planning and risk review before implementation. For broader sourcing context, consider medical device contract manufacturing services and the quality-system considerations involved.
The single-source vs multi-vendor medical device manufacturing decision should reflect both product needs and your organization’s governance capacity. Fong’s supports medical device development and manufacturing across defined project scopes. Discuss your device manufacturing requirements with the team to explore an approach aligned to your portfolio.
How an integrated CDMO can support a single-source strategy
A single-source strategy can place selected development and manufacturing activities with one CDMO, creating a coordinated scope across stages that would otherwise involve separate handoffs. The scope might include design support, prototyping, validation, assembly, testing, and production, or only a defined subset. Integration can help teams manage interfaces within that scope, but it doesn’t remove the need to establish decision rights, quality responsibilities, and customer oversight.
Fong’s Engineering & Manufacturing provides end-to-end medical device development and manufacturing, with capabilities that include precision machining, laser processing, cleanroom assembly, testing, and packaging. Its smart manufacturing lines include real-time monitoring and automated inspection. These capabilities do not promise a particular project result; assess how they align with the device’s processes and defined requirements.
From engineering handoff to controlled production
Connecting engineering and manufacturing activities can help teams address design-for-manufacture considerations while product requirements and production methods are being developed. For example, a design change may affect component manufacture, assembly sequence, or inspection needs. Early communication across those functions makes the impact visible before a process is transferred into production. The scope and approval responsibilities for each decision should still be documented.
Validation planning is another interface to define. Fong’s uses process validation frameworks including IQ, OQ, and PQ. Teams can determine which processes require validation, what evidence will be generated, and who reviews or approves it within the project’s quality arrangements. Validation records should remain linked to the equipment, process, and scope they cover.
Assess fit through project scope and accountability
An integrated CDMO is one sourcing option to evaluate, not a universal recommendation. Assess the device type, lifecycle stage, critical processes, quality requirements, and responsibilities your organization intends to retain. A focused scope can be appropriate where a specialist activity is needed; broader coordination may suit projects where several engineering and production stages depend on closely managed interfaces.
Before defining the arrangement, clarify:
- Scope: Which development, manufacturing, assembly, testing, or packaging activities are included?
- Accountability: Who owns specifications, change decisions, nonconformance communication, and approval of records?
- Interfaces: How will engineering information and validation evidence move between project teams?
- Oversight: What quality reviews and performance measures will the customer maintain?
The choice in single-source vs multi-vendor medical device manufacturing depends on whether the proposed scope, capabilities, and governance fit the portfolio. A project discussion can bring those requirements into focus. Discuss your medical device manufacturing project with Fong’s to explore CDMO support aligned to its lifecycle and quality needs.
Set your sourcing model up for the next lifecycle stage
A sourcing decision can be revisited as a device moves from development into production or as portfolio requirements change. Treat the operating model as part of lifecycle planning: define what should remain integrated, where specialist suppliers add value, and how responsibilities will be reviewed when the scope evolves. This gives engineering, quality, and procurement teams a shared basis for adjusting the structure without losing accountability.
Fong’s brings more than 40 years of medical device manufacturing experience, an ISO 13485 quality system, and documented IQ, OQ, and PQ validation frameworks. Its capabilities also include Class 8 cleanroom assembly and smart manufacturing. These credentials and capabilities can inform an evaluation of whether an integrated scope fits your device and oversight needs; they don’t make one sourcing model right for every portfolio.
Use your next planning cycle to turn the single-source vs multi-vendor medical device manufacturing decision into a defined scope, with responsibilities and interfaces that can be governed over time. Discuss your medical device manufacturing requirements with Fong’s and explore an approach aligned to your project. A clear starting point can support confident planning for the work ahead.
Frequently Asked Questions
Is single-source medical device manufacturing always more efficient?
No. The efficiency of single-source vs multi-vendor medical device manufacturing depends on the work assigned and how decisions are managed. One supplier may simplify coordination if it handles connected stages, but internal reviews, approvals, and supplier oversight still take time. Compare how a design revision would be assessed and implemented under each model. Map the people, records, and approvals involved before treating supplier consolidation as an efficiency gain.
Can a medical device manufacturer use both single-source and multi-vendor models?
Yes. A company can assign a defined package to a lead CDMO while sourcing a specialized component or process separately. For instance, the lead partner could manage an agreed production scope while the device company retains a specialist supplier for a distinct activity. Document who controls specifications, owns records, communicates changes, and resolves interface issues. This hybrid arrangement can align sourcing with technical needs, provided cross-supplier governance is explicit.
How do you reduce risk when relying on one medical device manufacturing supplier?
Begin with a dependency map that identifies critical processes, materials, equipment, capacity, and knowledge held by the supplier. Then define how disruptions are escalated, what information the customer can access, and who assesses recovery options. Evaluate a possible alternative against the controlled process and its qualification needs rather than assuming it is ready for use. These measures strengthen preparedness, but they cannot eliminate supplier dependency or guarantee continuous supply.
Does using multiple vendors make medical device quality harder to manage?
It can make coordination more demanding, particularly if suppliers use different record flows or change-notification processes. That does not make the model inherently lower quality. Establish a common interface package for each handoff, including the applicable specification revision, acceptance evidence, and route for reporting a nonconformance. Assign an owner to reconcile information across suppliers so gaps are identified before they affect downstream work.
What should a sourcing comparison include beyond the number of suppliers?
Compare the actual work allocation, process capability, responsibility for records, change authority, continuity dependencies, and your team’s oversight capacity. Also examine how the arrangement handles a design revision or a rejected component, since those events test the interfaces in practice. Record assumptions alongside the comparison. This helps distinguish a need for a specialized capability from a preference for consolidation, and makes the reasoning useful across products in the portfolio.
Can one CDMO support medical device development and manufacturing?
Yes. A CDMO can take responsibility for a defined set of development and manufacturing activities, with boundaries tailored to the project. Fong’s Engineering & Manufacturing provides CDMO services for medical device projects, and the scope can be discussed in terms of product needs, lifecycle stage, deliverables, and quality responsibilities. The customer retains a role in defining requirements and oversight, even when a partner coordinates multiple activities.